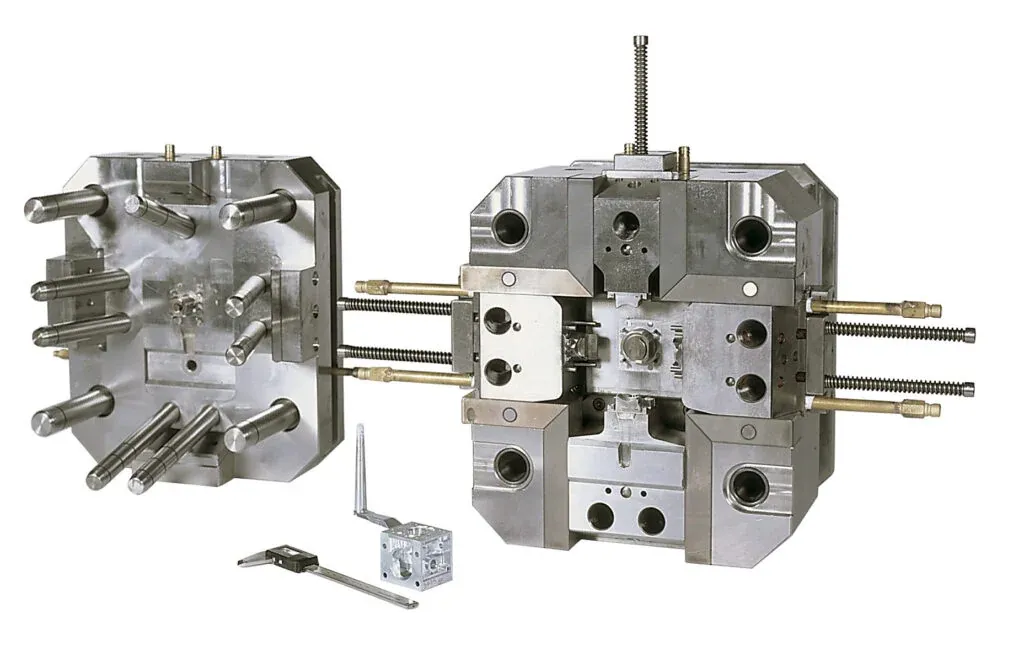
Offshore tooling can work very well. When it goes wrong, the cause is rarely the steel or the machining. More often it is a simpler question that nobody answered at the start of the program: who is allowed to tell the tool shop to change the tool?
The case: instructions from outside the channel
Bob Gray was tooling lead for a Tier 1 automotive supplier on a Tesla Model 3 program. The program ran through a chain the OEM required: the Tier 1 supplier, a contract molder in Mexico, then a tool shop in China.
A Tesla surface (texture) engineer went straight to the tool shop and directed changes to the tools. The modified tools produced bad parts. Bob was flown to China at a day's notice.
On site, he took control of the program and spent three days getting direction back into one channel. He made clear to the molder and the tool shop that they take instructions only from the supplier that owns the program.
Then came the damage. A leather-grain textured cavity had been weld-repaired without color-match welding. The weld showed through on every molded part, a visual defect the OEM would never accept.
Bob took the program to PPAP with the damaged cavity as a short-term measure and had the tool shop build a new cavity with the correct texture. It reached the molder about two months after PPAP. The program passed PPAP, and the OEM approved the parts while the permanent cavity was built. Read the full case study.
Why a weld shows through texture
Texture is etched into the steel, and the etch reacts to the steel it meets. When a cavity is welded with a filler that does not match the base steel, the repaired area can etch differently from the steel around it. On the molded part that shows as a patch with a different grain or gloss.
On a leather grain there is nowhere to hide it. Every part carries the mark, in the same place, in a surface the customer looks at. That is why weld repairs on textured cavities have to be planned and approved, not improvised.
The real failure was the channel
A tool shop that receives instructions from its customer's customer is in a difficult position. Without a clear rule, it will usually do what it is told by the person who seems to have the most authority.
That is why the first three days on site went on getting direction back into one channel. Until instructions flow through one channel, any repair can be undone by the next instruction. The technical recovery could only start once that was settled.
Set the rules before the purchase order
The time to decide who can change the steel is before the tool is ordered, in writing, with every party in the chain.
- One owner. Name the person who can authorize a steel change. Everyone else, including the end customer, gives input to that person.
- Written changes only. No steel is cut, welded or textured on a verbal instruction or a message from someone outside the channel.
- Texture comes last. Dimensional and functional approval first. Any change after texture needs its own sign-off.
- A repair standard. Weld repairs on cosmetic or textured surfaces are approved in advance, with the material and the method stated.
- Review checkpoints. A design review before steel is cut, progress checks during the build, and a trial before the tool ships.
None of this is complicated. It is simply easier to agree at the start than in the middle of a problem.
When it has already gone wrong
The recovery in this case followed an order worth copying.
- Get control of the instructions first. Nothing else holds until the channel is clear.
- Find out exactly what was changed. Inspect the tool and the parts yourself. Do not rely on a summary.
- Separate the short-term path from the permanent fix. Here, the program went to PPAP on the damaged cavity as a short-term measure while a new cavity was built.
- Agree both paths with the customer, so the short-term parts are approved and the permanent fix has a date.
The alternative is to stop the program until a new textured cavity arrives. In this case the permanent cavity reached the molder about two months after PPAP, with approved parts running in the meantime.
What it means for sourcing
None of this is an argument against offshore tooling. Domestic builders offer shorter lead times and easier communication. Offshore builders can reduce cost on larger tools. Either can deliver a good mold, and either can go wrong when control is unclear.
The lesson is about ownership. On offshore programs, steel changes must go through the program owner. Clear channels prevent damage that can take months to undo.
If you are quoting a new mold, comparing builders, or trying to get a program back on track, that is what mold sourcing and quoting help covers: the specification, the quote comparison, the choice of builder, and oversight through the build. Start with a free 15-minute call.
Founder of BG Innovations LLC. 45+ years in injection molds, with programs for BMW, Tesla, Honda, GE Appliances and Motorola.